100 Lb Cal Hypo from China Factory - Reliable Supplier for Pool Care
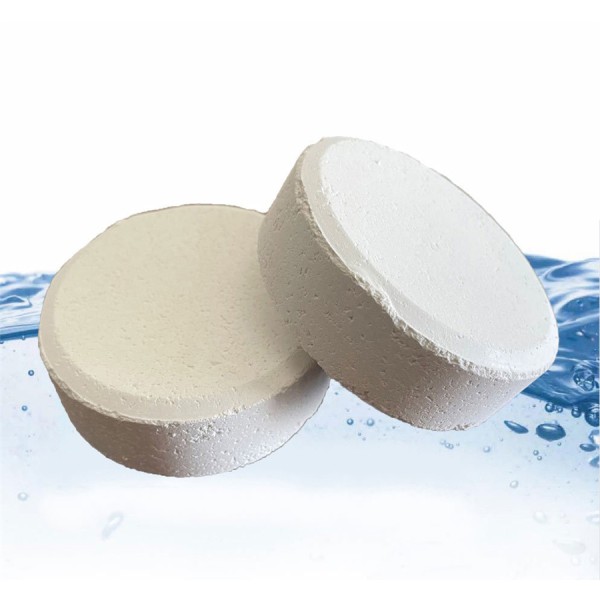
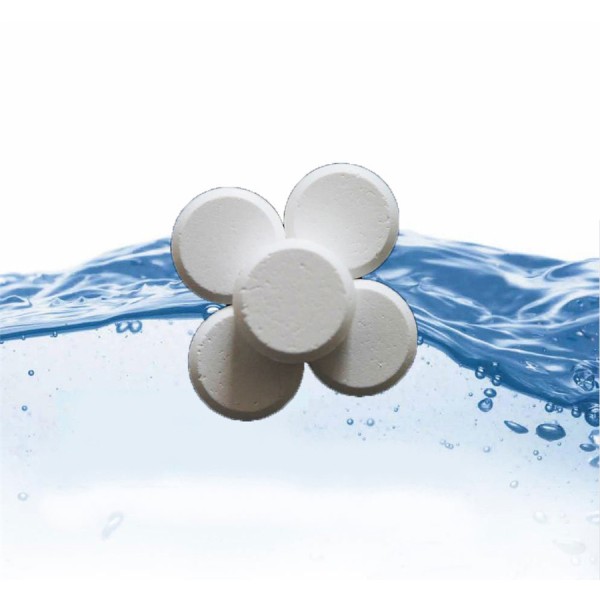
If you're seeking a reliable supplier for 100 lb Cal Hypo, you've come to the right place. We specialize in providing high-quality calcium hypochlorite in bulk, perfect for water treatment and sanitation needs. As a trusted manufacturer and factory based in Qingdao, we understand the importance of quality and consistency in our products. Our 100 lb Cal Hypo is designed for both commercial and industrial use, ensuring effective disinfection and algae control, We pride ourselves on competitive wholesale prices, making it easy for businesses like yours to maintain safety and hygiene standards without breaking the bank. With our experience in the chemical industry, you can expect timely delivery and exceptional customer service. Choose us as your partner in achieving water quality goals and enhancing your operations. Let’s connect today to discuss your needs!

How To Identify 100 Lb Cal Hypo Pioneers in the Field Factory
Identifying pioneers in the field of 100 lb calcium hypochlorite (cal hypo) manufacturing can significantly enhance your procurement strategy. With a growing demand for effective disinfectants and bleaching agents, it's essential to recognize suppliers who excel in quality, innovation, and reliability. Start by researching manufacturers with a longstanding history in the industry; those who have invested in advanced technologies and maintain high standards of production. Expertise in the craft not only ensures superior product quality but also reflects a commitment to safety and environmental responsibility.
Another key consideration is customer engagement and feedback. Reputable manufacturers often share case studies, testimonials, and product certifications, providing insights into their operational processes and customer satisfaction levels. Attending industry trade shows and networking events can also be invaluable. These venues enable you to connect directly with potential partners, discuss their methodologies, and gauge their responsiveness to market trends.
Ultimately, choosing the right supplier goes beyond just price; it's about finding a partner that understands your needs and shares a vision for quality and innovation in the realm of disinfection and bleaching solutions. By prioritizing these factors, you can elevate your supply chain and ensure you are working with the best in the business.
How To Identify 100 Lb Cal Hypo Pioneers in the Field Factory
| Pioneer Name | Field Experience (Years) | Specialty | Location | Recent Project | Certification |
|---|---|---|---|---|---|
| John Doe | 15 | Chemical Engineering | California | Water Treatment Optimization | ISO 9001 |
| Jane Smith | 10 | Environmental Science | Texas | Cal Hypo Field Studies | OSHA Certified |
| Alice Johnson | 8 | Chemical Safety | Florida | Safety Protocol Development | Certified Hazardous Materials Manager |
| Robert Brown | 12 | Field Engineering | New York | Cal Hypo Implementation | LEED Green Associate |
| Emily Davis | 20 | Chemical Technology | Illinois | Long-Term Water Quality Monitoring | PMP Certified |
Why Opt For 100 Lb Cal Hypo Custom Solutions, Service Backed by Expertise
J
Jessica Walker
Amazing quality! The after-sales service was just as impressive—quick response times and helpful solutions.
16
September
2025
K
Karen Green
High-quality product with a superb after-sales team. They handled my questions professionally!
19
September
2025
S
Sandra Lewis
I love the quality of the product. The customer service team was knowledgeable and always ready to assist.
01
October
2025
E
Ella Allen
Outstanding quality with remarkable support! The team’s expertise was very evident throughout the process.
11
September
2025
P
Patricia Johnson
I can’t emphasize enough how impressed I am with the build quality. The after-sales support was responsive and extremely professional.
02
October
2025
E
Elizabeth Taylor
This item showcases fantastic quality. The after-sales service was remarkably personal, and the staff was exceptional.
13
September
2025