Innovations and Application Trends of Calcium Hypochlorite in Modern Water Treatment
As global industrialization accelerates and public health standards continue to rise, Calcium Hypochlorite (Cal Hypo)—the cornerstone of high-performance disinfectants—is undergoing a technical revolution centered on high purity, stability, and low residue.
Industrial Upgrading: From Traditional Methods to High-Purity Sodium Process
In the water treatment chemical market, Calcium Hypochlorite in water treatment is preferred for its high available chlorine content and convenient storage. Recent market trends indicate that the high-quality "Sodium Process" is increasingly becoming the mainstream for high-end applications.
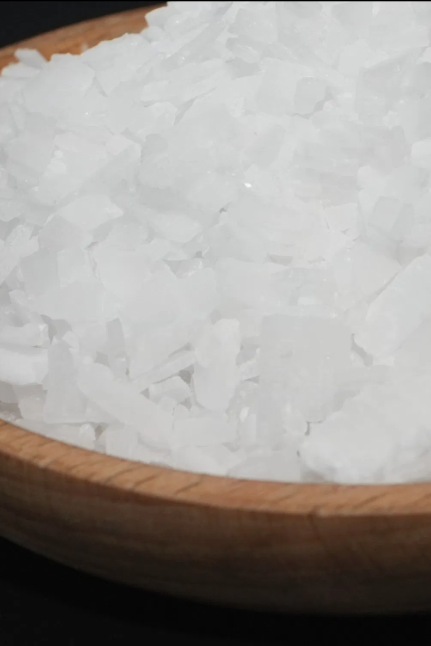
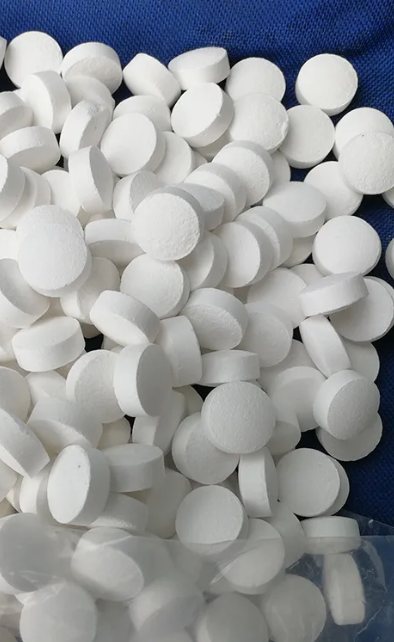
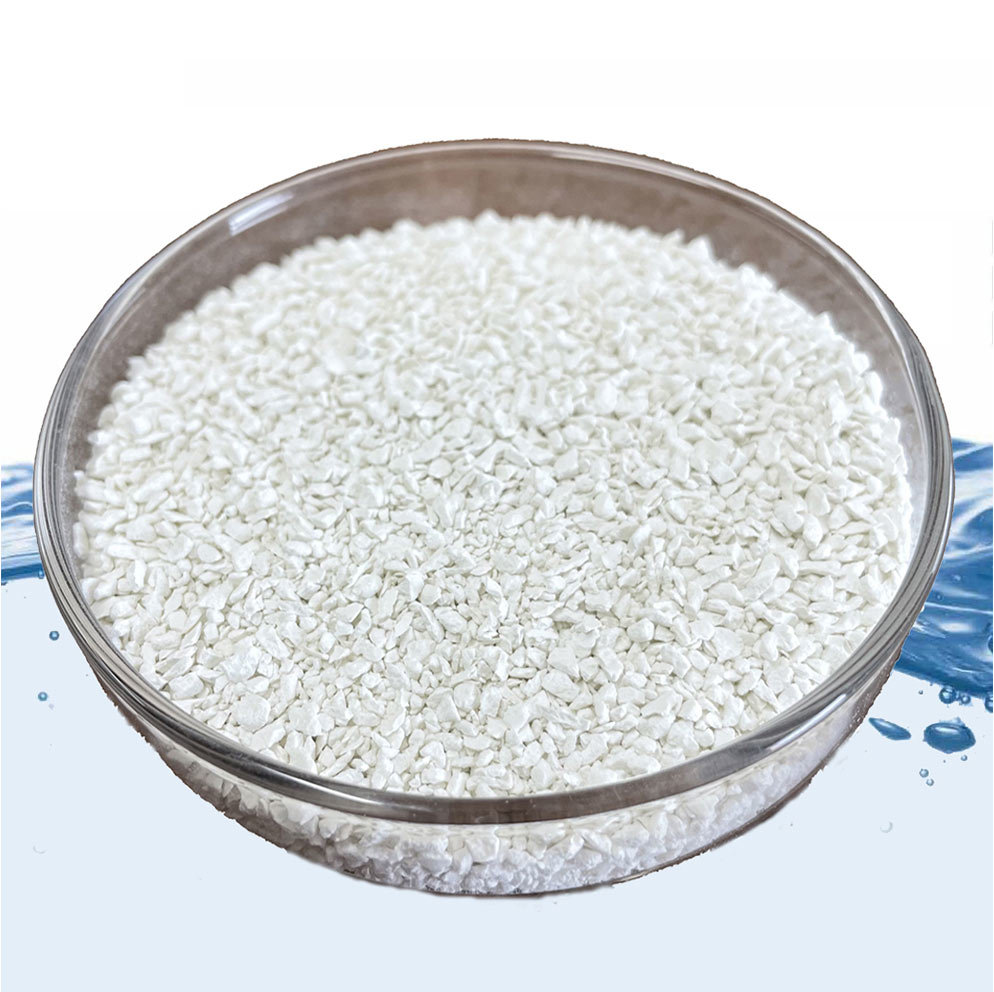
Compared to traditional methods, Solid Calcium Hypochlorite produced via the advanced sodium process exhibits superior chemical stability. This ensures a significantly lower degradation rate of available chlorine during long-term storage and high-temperature transport. Furthermore, its minimal impurity level (low water-insoluble matter) prevents clogging in automated dosing systems, greatly enhancing operational efficiency in industrial settings.
Multi-Dimensional Applications: Building a Full-Scenario Purification System
The efficacy of Ca(ClO)₂ has long surpassed simple bleaching. In today's global health environment, it demonstrates remarkable versatility across multiple sectors:
-
Drinking Water Safety: In regions with limited infrastructure or during emergency relief, Calcium Hypochlorite for drinking water disinfection remains the most economical and reliable defense line, ensuring biological safety for residents.
-
Pool and Spa Maintenance: It effectively inactivates viruses, bacteria, and stubborn algae while maintaining water clarity, making it a core chemical for international standard swimming facilities.
-
Livestock and Food Processing: When used as a Calcium Hypochlorite cleaning solution, it provides broad-spectrum sterilization for livestock housing and food contact surfaces without leaving unwanted odors, meeting stringent biosecurity requirements.
Environmental Impact: Breakthroughs in Granulation Technology
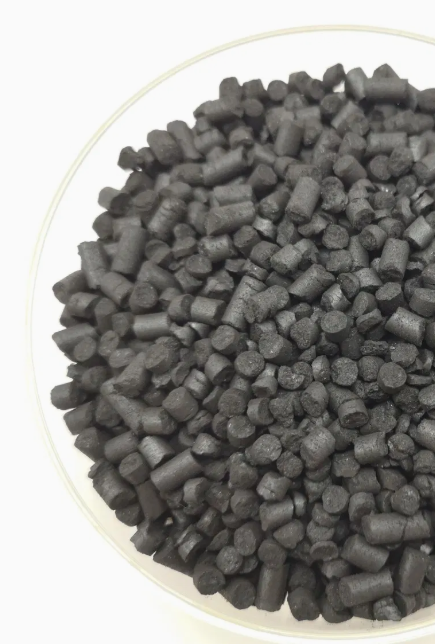
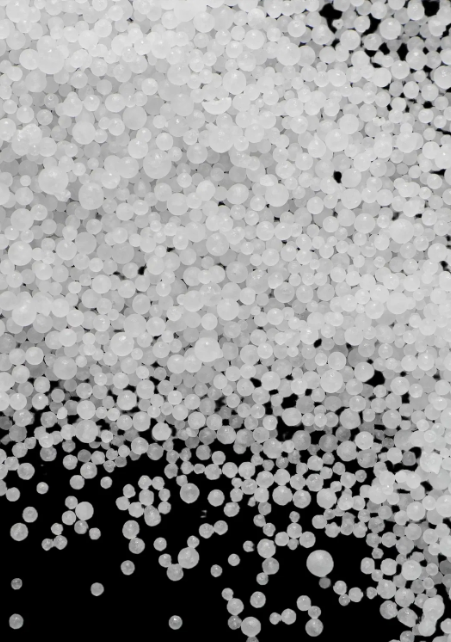
Modern chemical manufacturing is focusing on improving the physical form of the product. By optimizing granulation techniques, dust pollution has been significantly reduced, protecting the respiratory health of operators. Additionally, specialized packaging developed for different climatic zones not only extends shelf life but also reduces chemical waste caused by product degradation.
Future Outlook: Integrating High-Quality Supply Chains with Global Standards
As global supply chains demand stricter compliance—such as EPA, ISO, and NSF certifications—only manufacturers who prioritize technological innovation and consistency in purity will lead the international market.
In the future, the use of Calcium Hypochlorite in water treatment will continue to evolve toward "precision dosing" and "green production." When integrated with automated sensors, it will serve as a critical component of smart water systems, providing scientific and precise chemical support for global public health.